Get a Free Quote

Our representative will contact you soon.
Name
Email
Tel
Company Name
Message
0/1000
medical blood bag manufacturer-0

Home > 

medical blood bag manufacturer

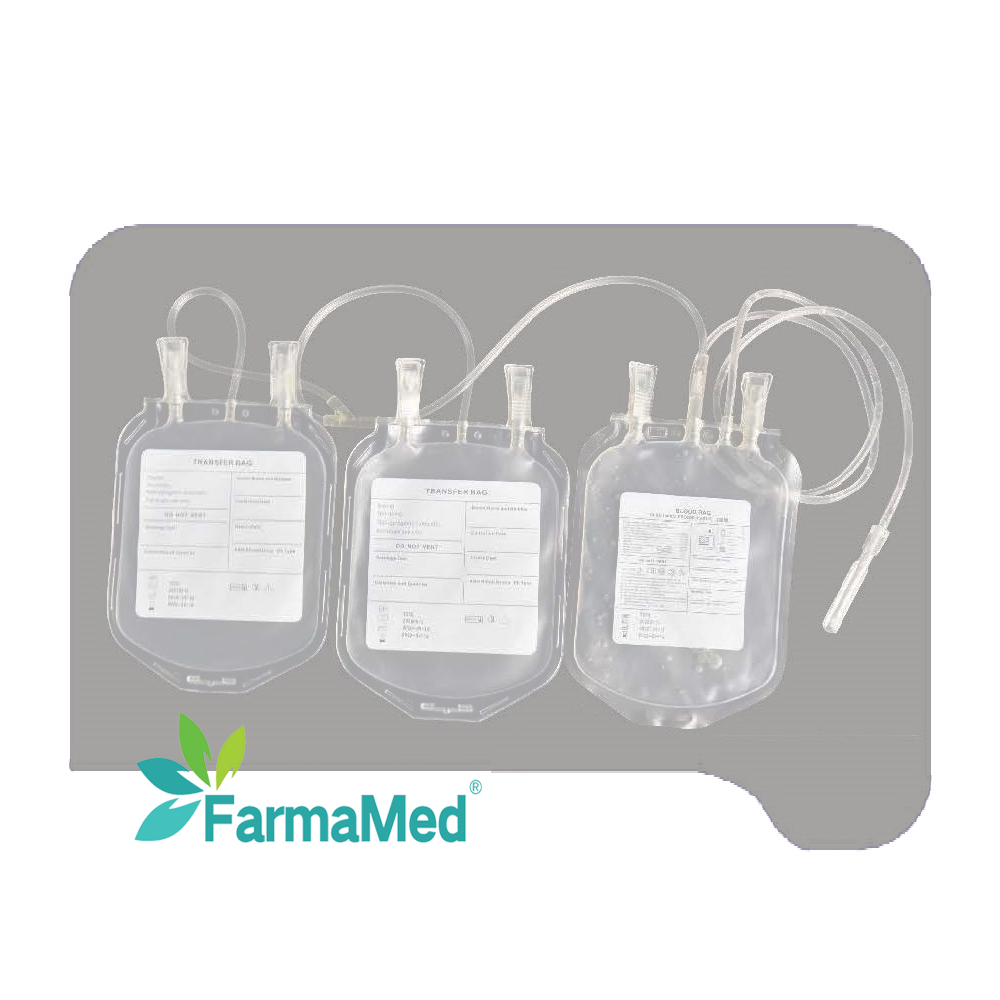
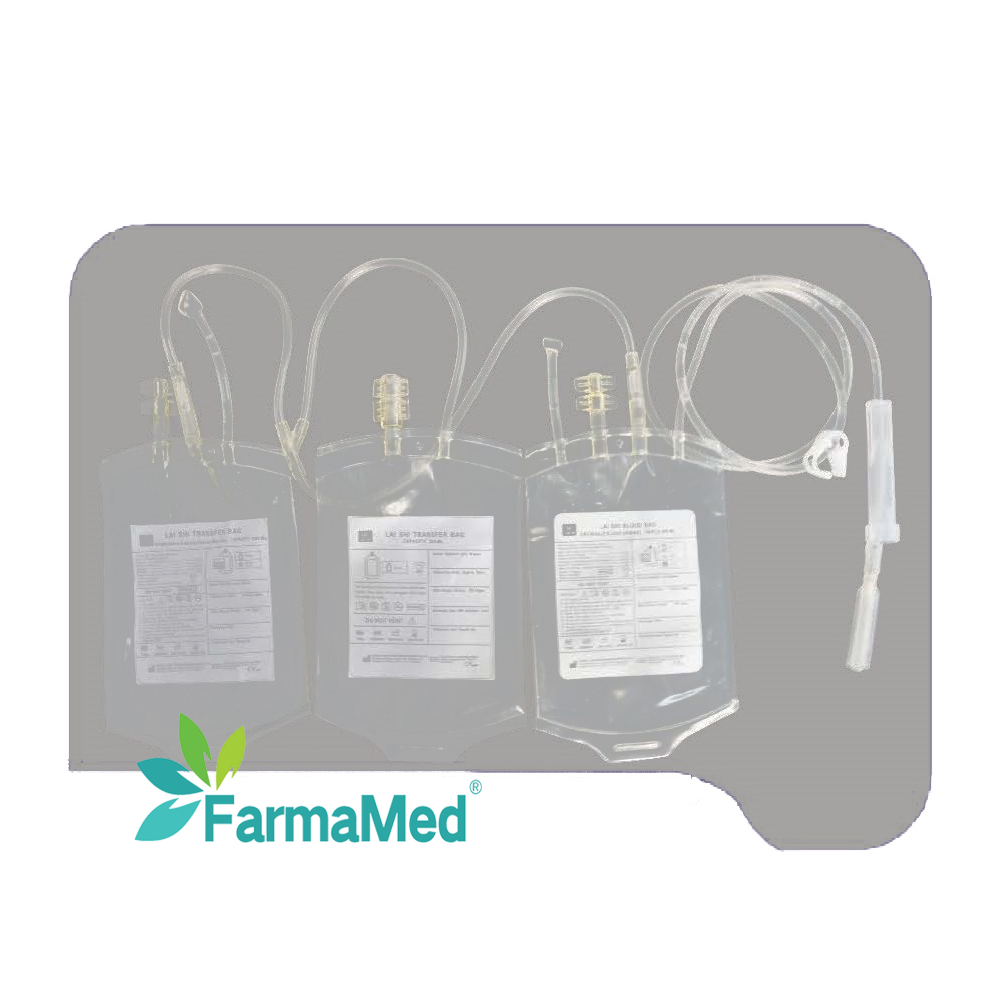
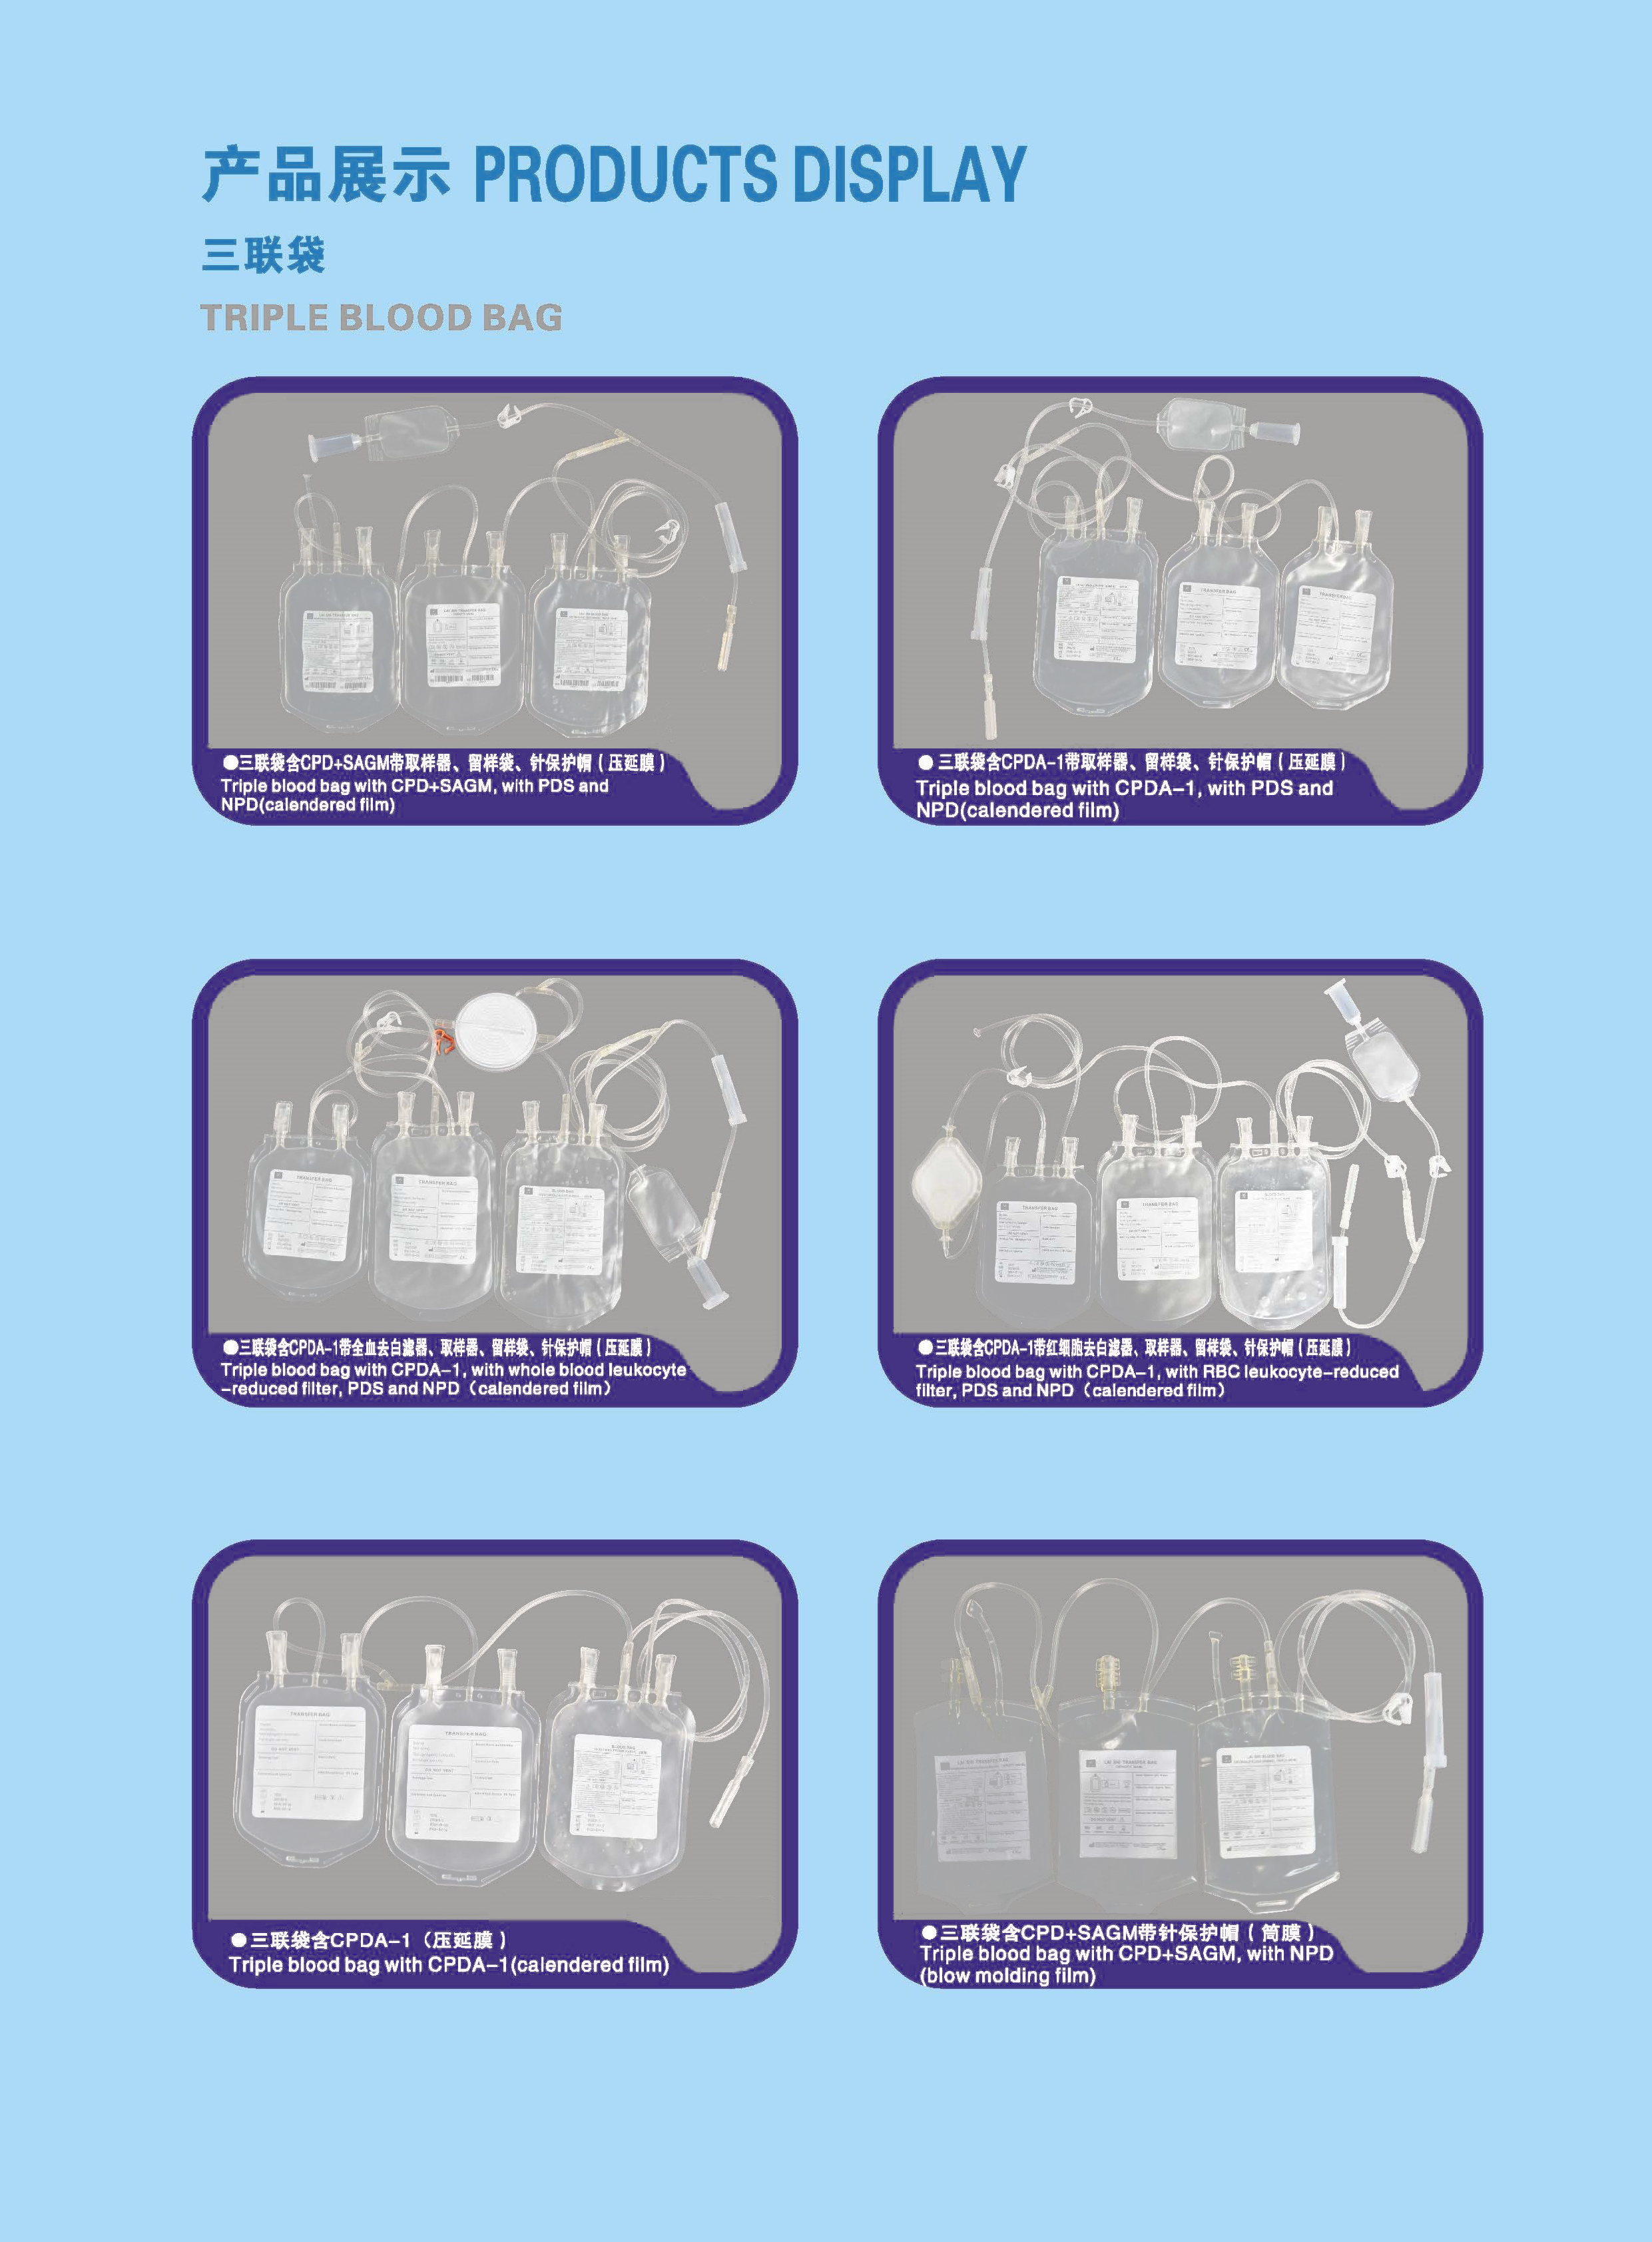
A medical blood bag manufacturer specializes in producing sterile, safe containers designed to collect, store, and transport blood and blood components. These essential medical devices are fundamental to healthcare systems worldwide, enabling blood banks, hospitals, and transfusion services to maintain critical blood supplies. The medical blood bag manufacturer creates products that meet stringent international safety standards, including FDA approval and ISO certifications, ensuring optimal performance in emergency and routine medical situations. Modern blood bags incorporate advanced technological features that protect blood integrity throughout the collection and storage process. The medical blood bag manufacturer integrates anticoagulant solutions, preservative additives, and specialized plastic materials that prevent contamination while maintaining cellular viability. These bags typically feature integrated tubing systems, needle assemblies, and sampling ports that streamline collection procedures and reduce infection risks. Applications for blood bags encompass whole blood collection, red blood cell separation, platelet concentration, plasma extraction, and therapeutic apheresis procedures. The medical blood bag manufacturer produces single, double, triple, and quadruple bag systems tailored to specific clinical needs. These products serve critical functions in trauma centers, surgical departments, oncology units, and regular donor centers. By providing reliable containment solutions, the medical blood bag manufacturer supports life-saving transfusions and emergency medical interventions globally.
New Product Releases

Choosing products from a reliable medical blood bag manufacturer delivers significant practical benefits for healthcare institutions and blood collection services. First, these manufacturers ensure superior safety standards that protect both patients and blood donors through rigorous quality control processes and compliant manufacturing protocols. Operational efficiency represents a major advantage when working with an established medical blood bag manufacturer. Their products feature user-friendly designs with clear labeling, integrated collection systems, and straightforward storage instructions that reduce training time for medical staff. This streamlined approach minimizes collection errors and accelerates donor processing, allowing facilities to increase blood supply capacity without compromising quality. Cost-effectiveness matters significantly for budget-conscious healthcare providers. A professional medical blood bag manufacturer offers competitive pricing through economies of scale while maintaining premium quality standards. Bulk purchasing options and consistent supply chains reduce procurement costs and storage expenses associated with inventory management. Product reliability ensures that blood components remain viable throughout extended storage periods. The medical blood bag manufacturer utilizes proven formulations and materials that preserve cell functionality, reduce hemolysis rates, and maintain optimal shelf-life characteristics. This directly impacts transfusion success rates and patient outcomes. Compatibility with existing equipment represents another crucial advantage. Blood bags from a reputable medical blood bag manufacturer integrate seamlessly with centrifuges, separators, and automated processing systems used in modern blood banks. This compatibility eliminates costly equipment modifications and training complications. Compliance support distinguishes quality manufacturers from competitors. A dependable medical blood bag manufacturer provides comprehensive documentation, regulatory assistance, and traceability records that satisfy inspection requirements and accreditation standards across different regions and healthcare systems.

Tips And Tricks

Anhydrous vs. trihydrate magnesium citrate: formulation selection and cost analysis.

01

Jun

Anhydrous vs. trihydrate magnesium citrate: formulation selection and cost analysis.

The selection between anhydrous and trihydrate forms of magnesium citrate represents a critical formulation decision that directly impacts product efficacy, manufacturing costs, and regulatory compliance for pharmaceutical and nutraceutical companies...
View More
How to qualify compliant OTC cream suppliers for tinea pedis and cruris treatment?

03

Aug

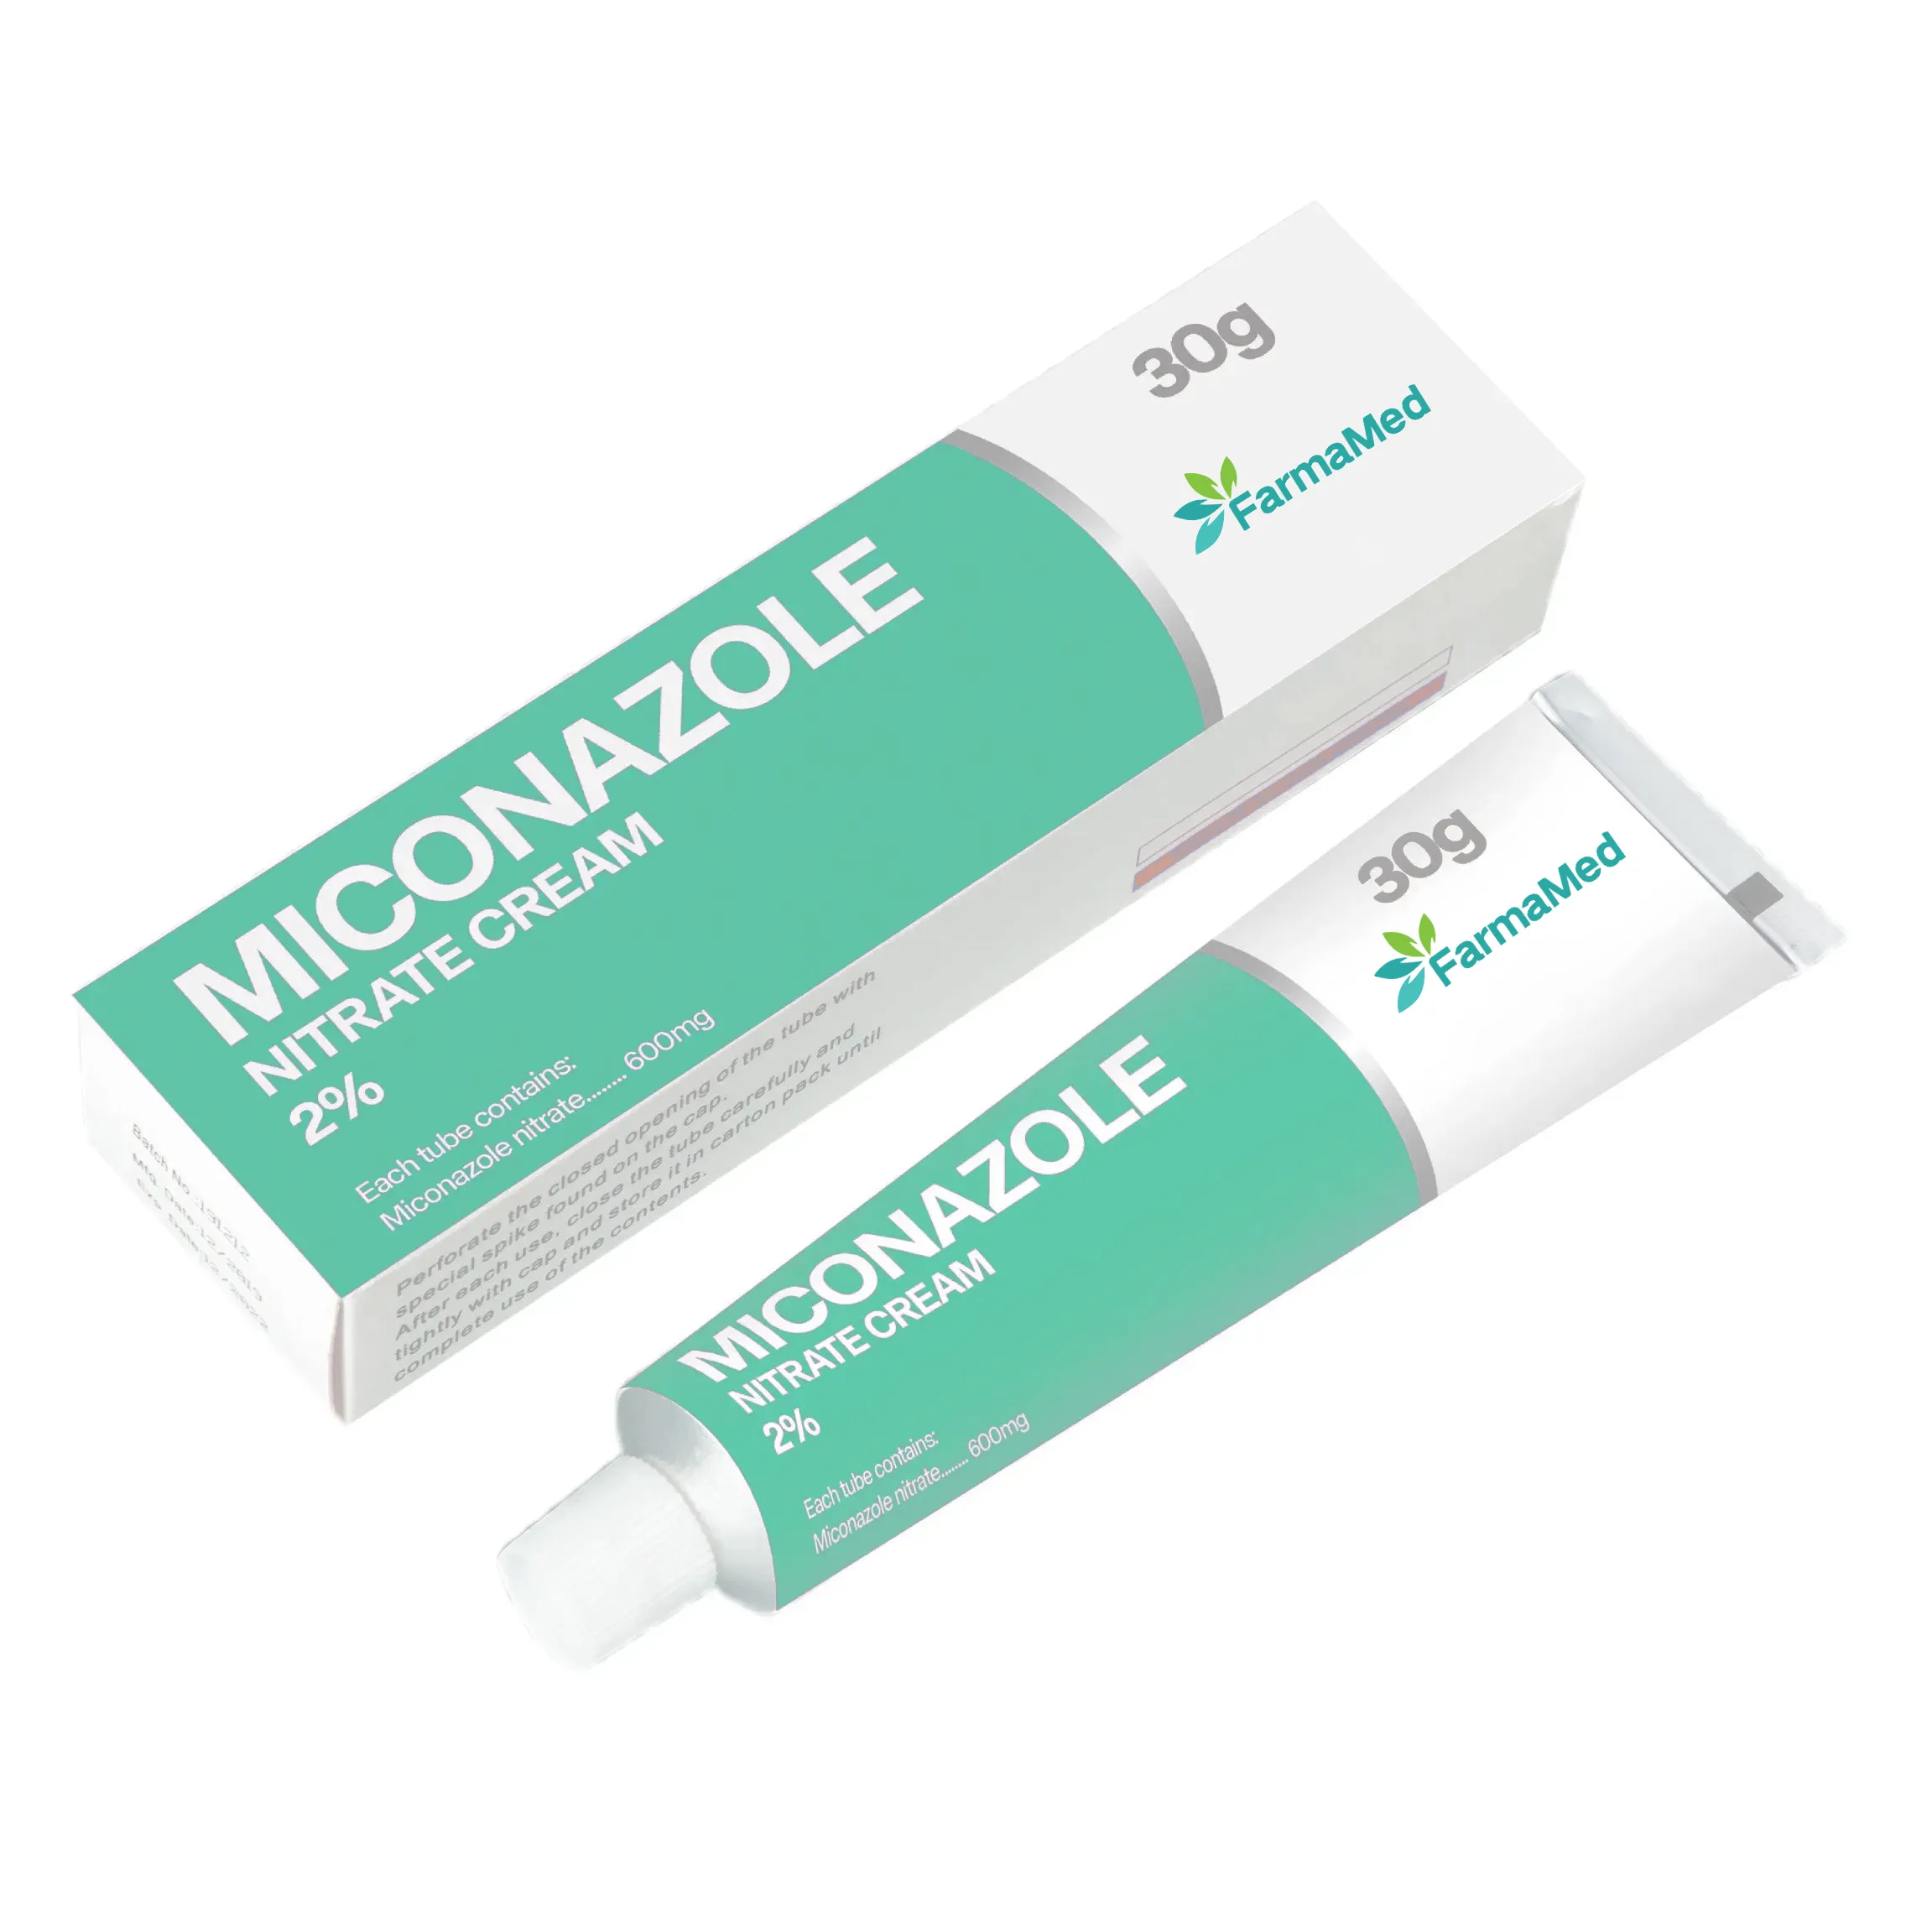
How to qualify compliant OTC cream suppliers for tinea pedis and cruris treatment?

Selecting the right supplier for miconazole cream requires a systematic approach that balances regulatory compliance, product quality, and reliability. Tinea pedis and tinea cruris are common fungal infections affecting millions of patients annually,...
View More
FDA registration pathway and OTC monograph compliance for eye drop exports to the US.

17

Aug

FDA registration pathway and OTC monograph compliance for eye drop exports to the US.

Exporting lubricant eye drops to the United States requires a thorough understanding of FDA regulations, OTC monograph standards, and compliance pathways. Manufacturers seeking to market lubricant eye drops in the US must navigate a complex regulator...
View More
How to verify batch consistency via MFR and density in bulk PP raw material procurement?

20

Aug

How to verify batch consistency via MFR and density in bulk PP raw material procurement?

Ensuring batch consistency in bulk procurement requires rigorous quality verification protocols. When sourcing white pp granules, manufacturers must implement standardized testing methods to confirm that each delivery meets established specifications...
View More

Get a Free Quote

Our representative will contact you soon.
Name
Email
Tel
Company Name
Message
0/1000

medical blood bag manufacturer

Advanced Safety and Sterility Assurance

Advanced Safety and Sterility Assurance

Leading medical blood bag manufacturers implement cutting-edge sterilization technologies and barrier protection systems that virtually eliminate contamination risks. Their products undergo rigorous microbiological testing, gamma irradiation sterilization, and validation procedures exceeding standard requirements. Each batch released by a professional medical blood bag manufacturer carries comprehensive documentation proving sterility and safety compliance. These advanced protective measures are critical because even minor contamination can render blood unusable and pose serious health risks to recipients. By maintaining exceptional safety standards, the medical blood bag manufacturer protects healthcare facilities from costly recalls, regulatory penalties, and patient safety incidents. The investment in superior safety infrastructure ultimately reduces overall healthcare costs through decreased complications and improved transfusion outcomes.
Extended Storage Capability and Blood Component Preservation

Extended Storage Capability and Blood Component Preservation

Premium blood bags from a reputable medical blood bag manufacturer incorporate scientifically formulated preservative solutions and oxygen-permeable materials that extend storage viability significantly. These innovations allow red blood cells to remain functional for up to forty-two days while maintaining cellular integrity and transfusion effectiveness. The medical blood bag manufacturer's careful material selection prevents gas exchange that degrades blood quality, ensuring that stored components meet transfusion standards throughout the entire shelf-life period. Extended storage capacity provides substantial operational flexibility, allowing blood banks to maintain adequate emergency reserves without frequent collection drives. This capability becomes invaluable during natural disasters, mass casualty events, and seasonal blood supply shortages. Healthcare facilities relying on quality products from a dependable medical blood bag manufacturer achieve superior inventory management and enhanced emergency preparedness.
Seamless Integration and Operational Compatibility

Seamless Integration and Operational Compatibility

Blood bags manufactured by industry-leading medical blood bag manufacturers are engineered for perfect compatibility with automated processing equipment, centrifuges, and separation systems used throughout modern blood banks. The standardized dimensions, tubing specifications, and port configurations ensure smooth operation without adapter modifications or system interruptions. This operational compatibility represents significant practical value because healthcare facilities can immediately implement products from a trusted medical blood bag manufacturer without costly equipment upgrades or workflow restructuring. Staff training requirements remain minimal since existing procedures transfer directly to new supplies. The medical blood bag manufacturer's commitment to standardization reduces human error, accelerates processing times, and increases overall departmental productivity. Facilities benefit from streamlined operations that maximize donor throughput while maintaining the highest quality standards throughout collection and processing procedures.

Get a Free Quote

Our representative will contact you soon.
Name
Email
Tel
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Name
Email
Tel
Company Name
Message
0/1000