Get a Free Quote

Our representative will contact you soon.
Name
Email
Tel
Company Name
Message
0/1000
blood bag manufacturer-0

Home > 

blood bag manufacturer

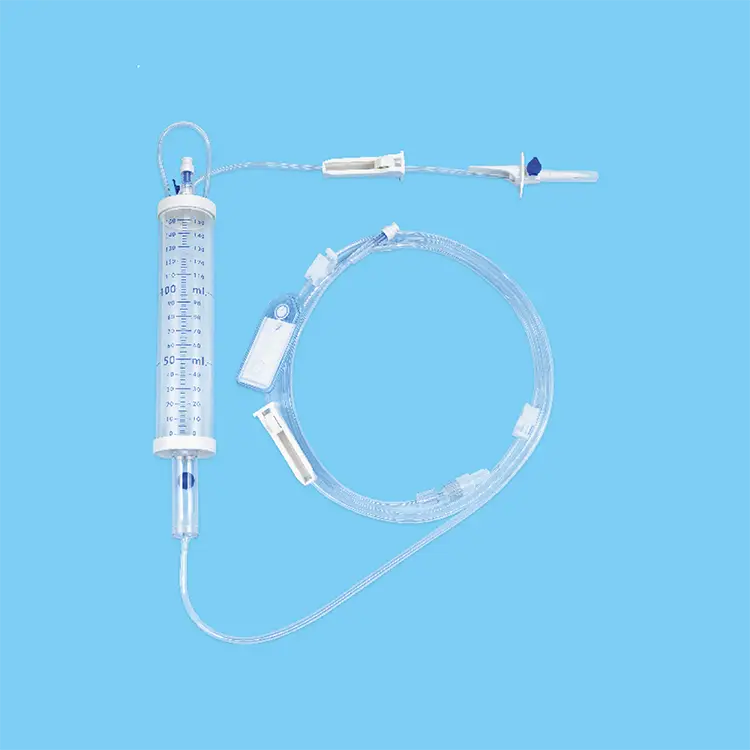
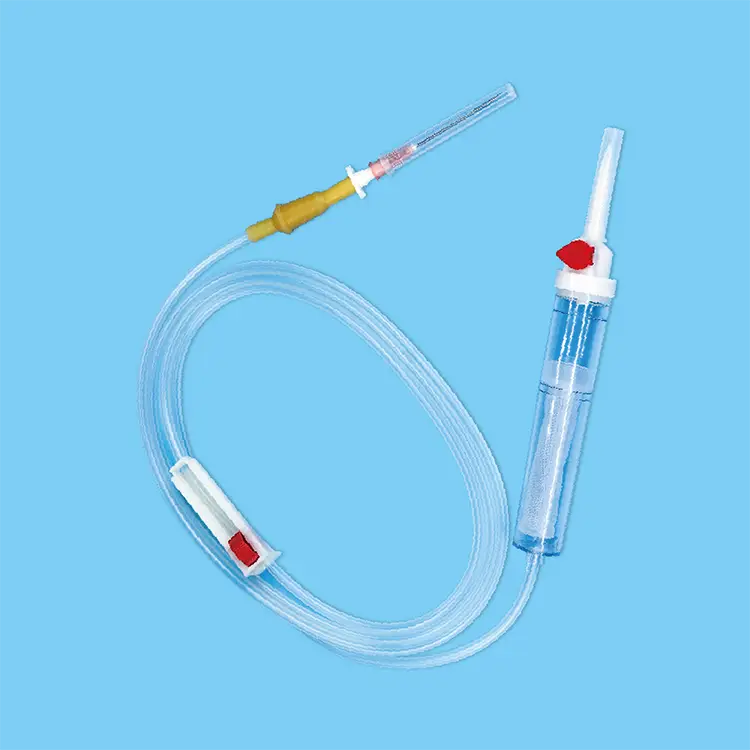
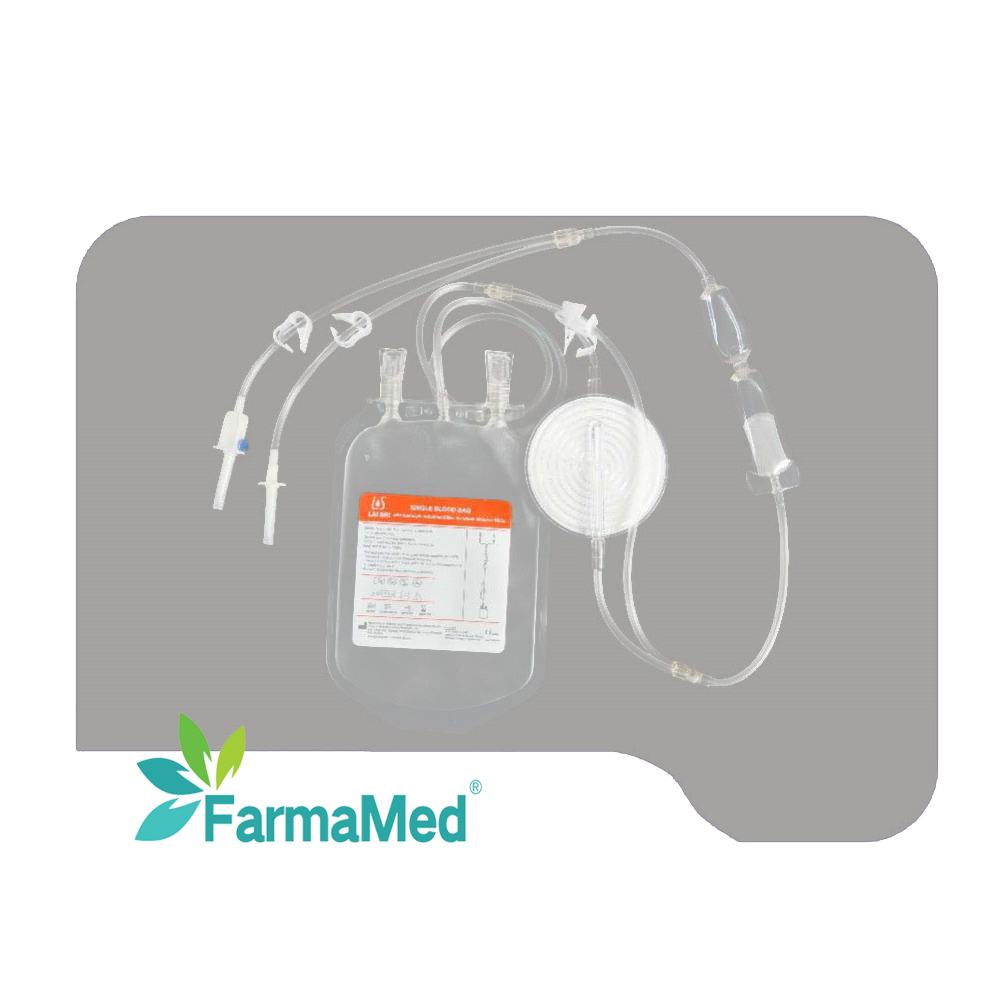
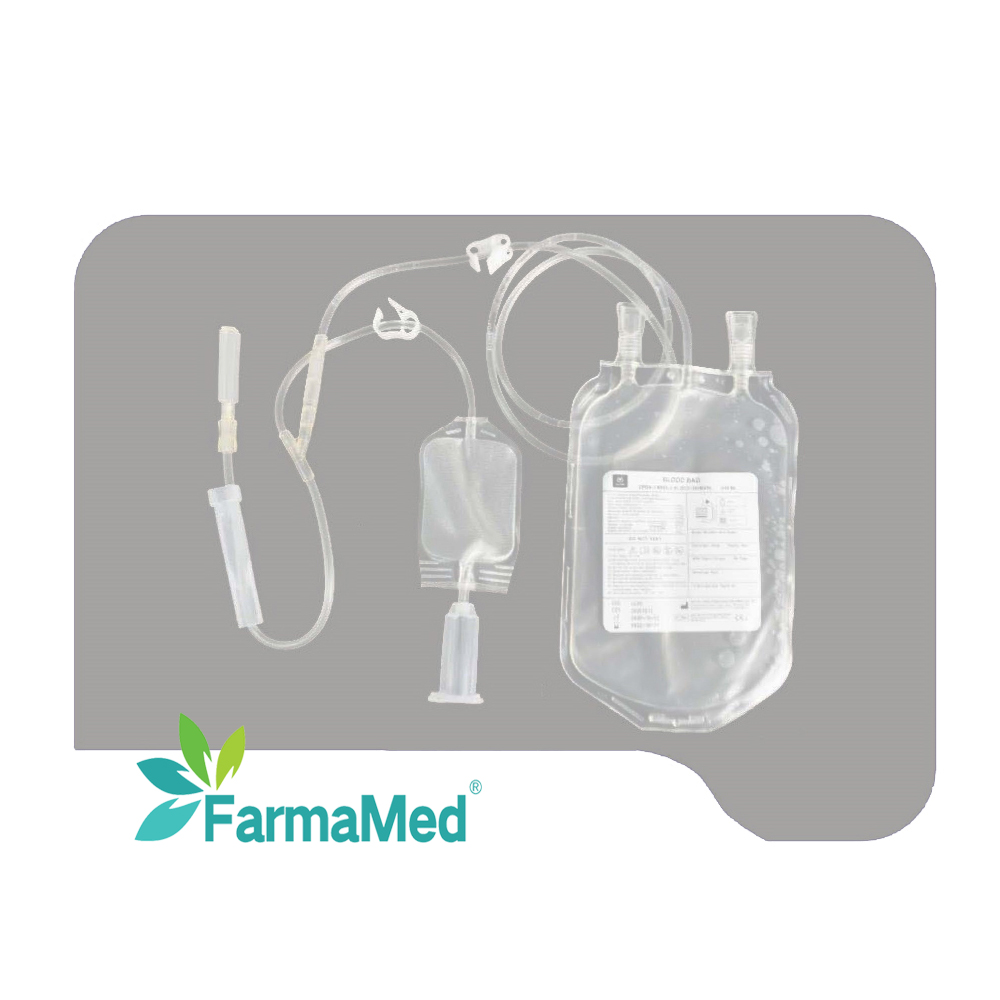
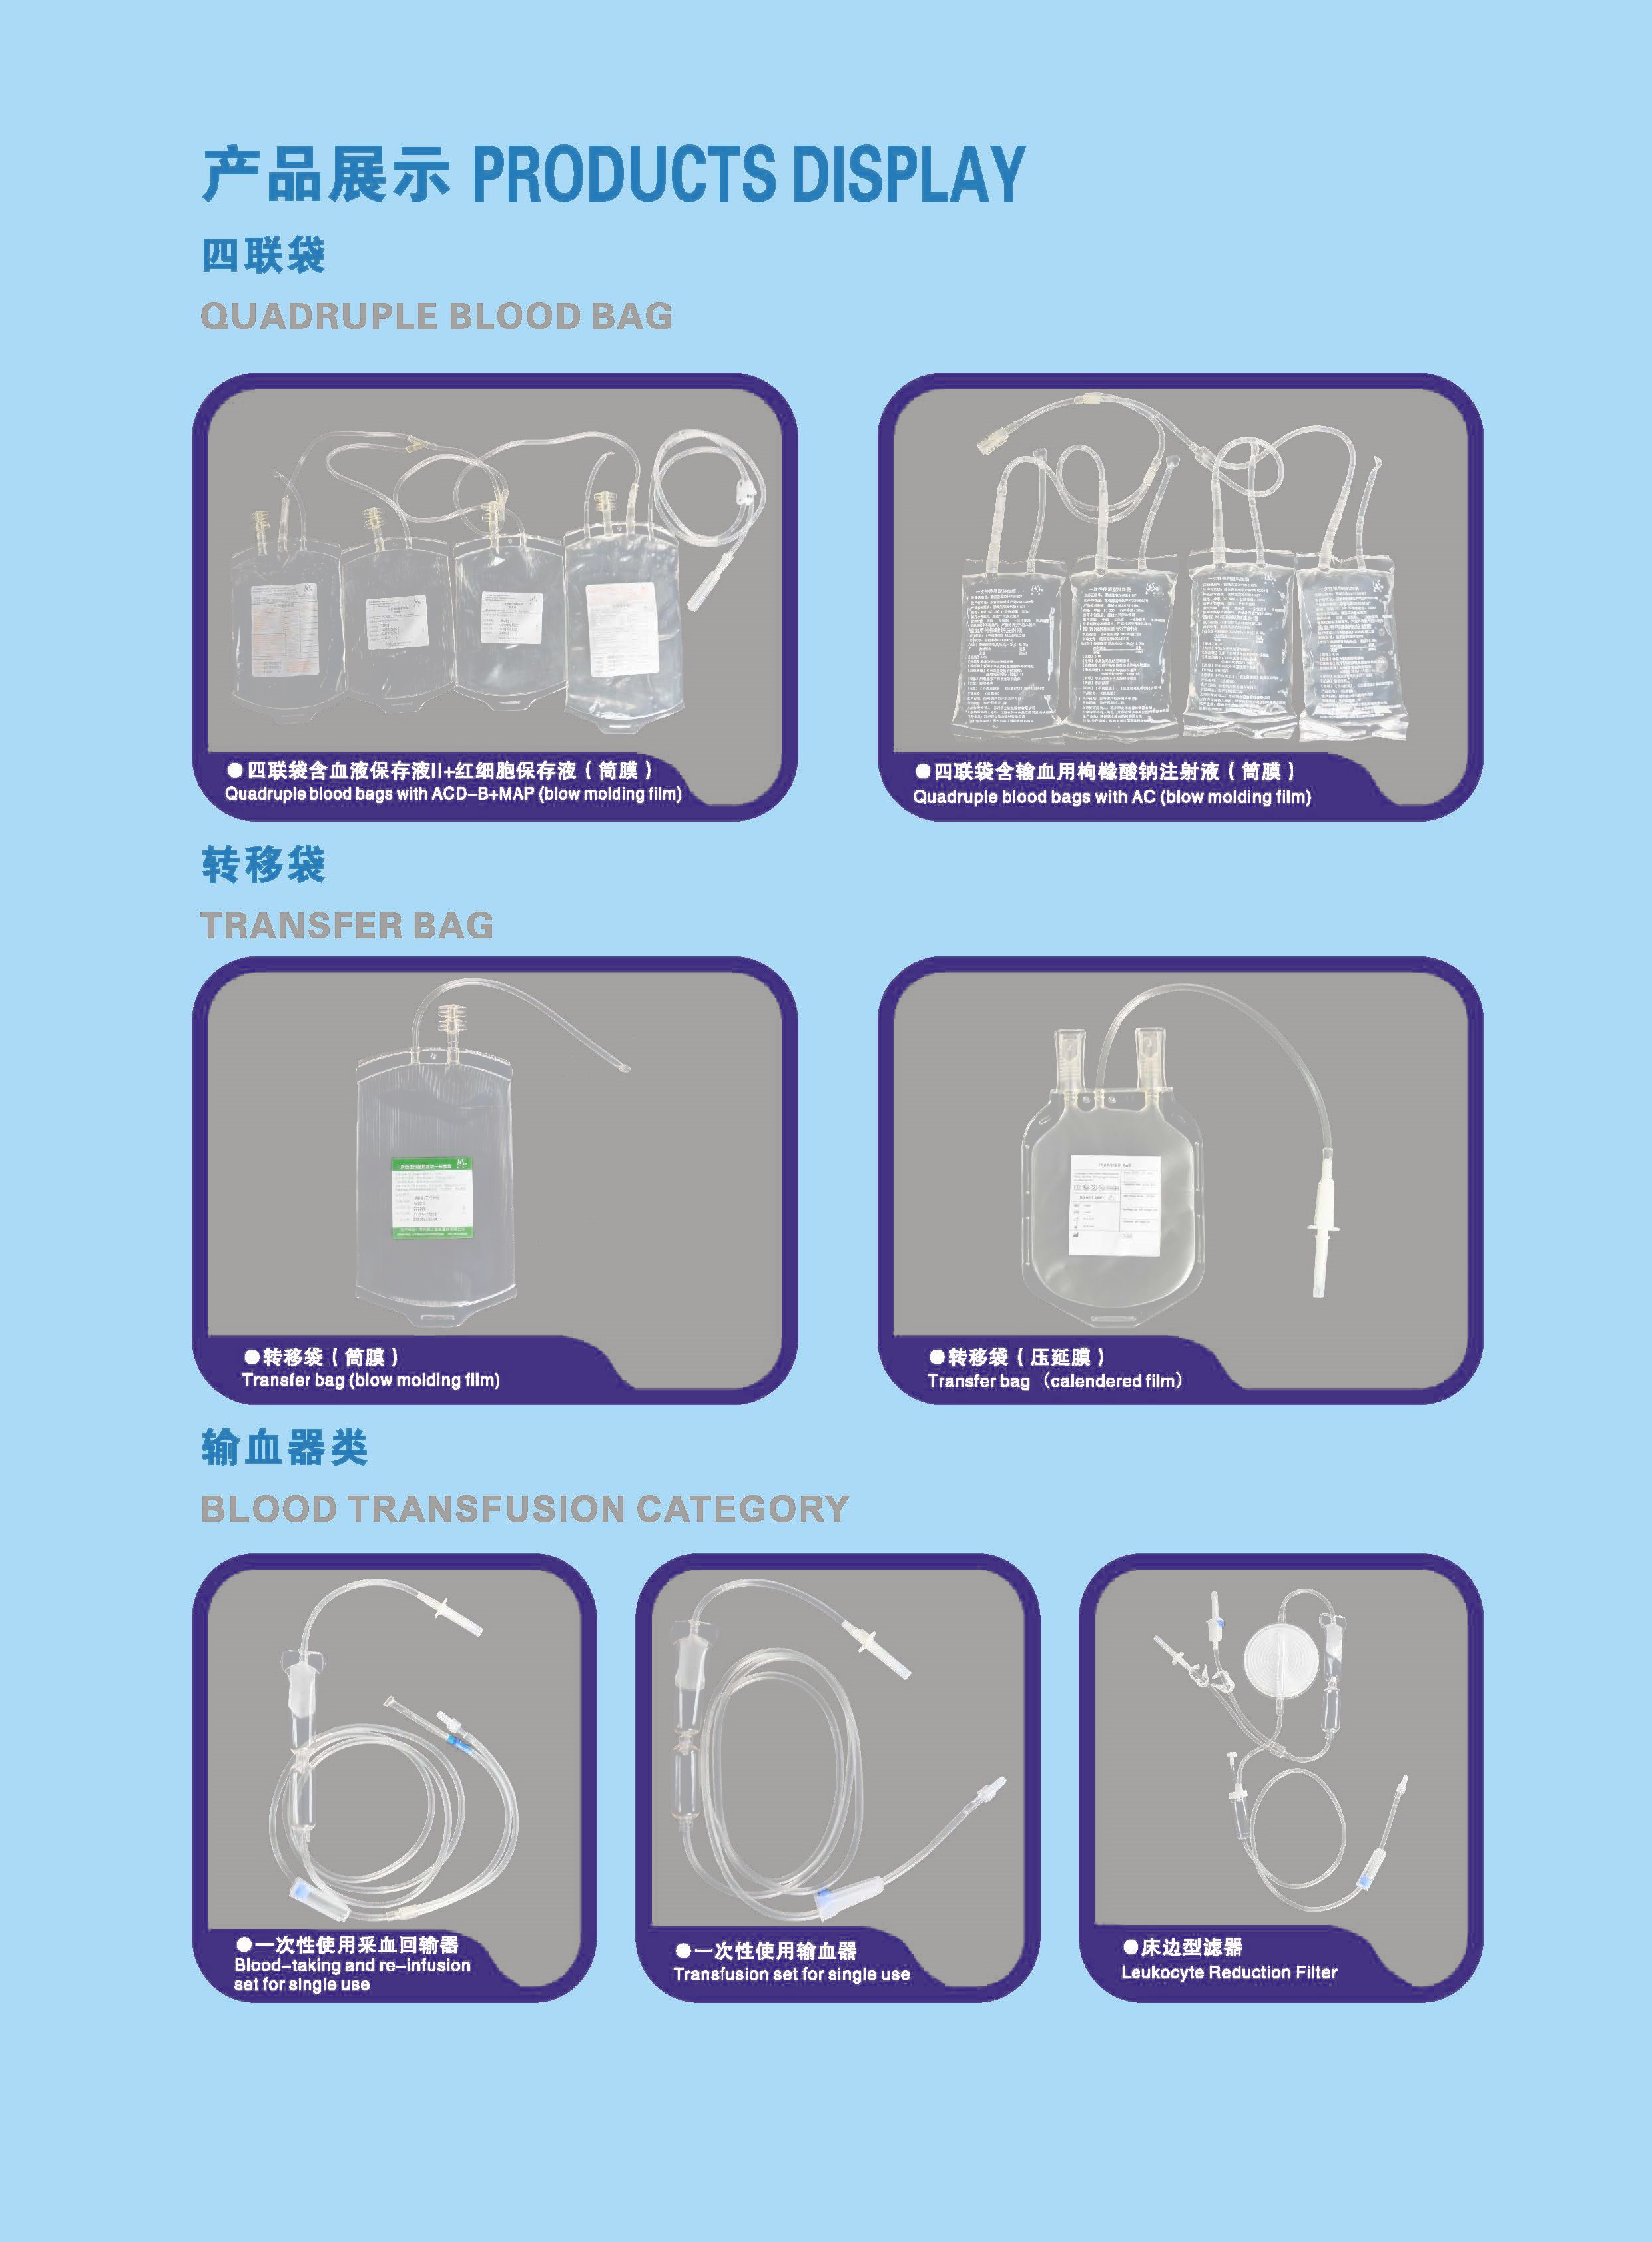
A blood bag manufacturer specializes in producing sterile, medical-grade containers designed for safe collection, storage, and transportation of blood and blood components. As a leading blood bag manufacturer, these companies develop essential products that meet rigorous international standards and regulatory requirements. Blood bags serve critical functions in healthcare systems, including whole blood collection, platelet separation, plasma storage, and red blood cell preservation. The blood bag manufacturer utilizes advanced materials such as PVC plasticizer-free compounds and food-grade plastics to ensure product safety and compatibility with various anticoagulants. Modern blood bag designs incorporate several technological features: integrated needle systems for efficient collection, sterile connection devices for component separation, and oxygen-permeable tubing for optimal preservation. These innovations distinguish a professional blood bag manufacturer from standard competitors. The collection bags typically contain anticoagulant solutions formulated to prevent clotting while maintaining cellular viability. Blood bag applications span across blood banks, hospitals, transfusion centers, and research facilities worldwide. A reliable blood bag manufacturer ensures compliance with FDA, CE, and ISO standards, guaranteeing product quality and safety. Advanced manufacturing processes enable proper sterilization through gamma radiation and ethylene oxide treatments. Temperature monitoring strips integrated into modern designs help maintain ideal storage conditions. The blood bag manufacturer continuously invests in research and development to improve preservation periods and reduce hemolysis rates, ensuring patients receive high-quality blood products for transfusions and medical procedures.
New Product Releases

Selecting a reputable blood bag manufacturer offers significant operational and clinical benefits for healthcare institutions. First, quality assurance ensures that every blood bag meets stringent international standards, reducing contamination risks and improving patient safety outcomes. A trusted blood bag manufacturer provides products with extended shelf life, allowing blood banks to optimize inventory management and reduce waste. The sterile connection systems developed by modern manufacturers enable safe component separation without compromising product integrity or introducing bacterial contamination. Healthcare facilities benefit from standardized designs that integrate seamlessly with existing transfusion protocols and equipment. Cost-effectiveness represents another advantage; efficient manufacturing processes and bulk purchasing from established blood bag manufacturers reduce per-unit expenses while maintaining premium quality. Training and technical support from the blood bag manufacturer enhance staff proficiency in proper handling and storage procedures. Advanced materials used by quality manufacturers ensure minimal interaction with stored blood, preserving cellular function and extending therapeutic effectiveness. Hospitals and blood banks gain competitive advantages by partnering with reputable blood bag manufacturers who continuously innovate preservation technologies. The reliability of a dedicated blood bag manufacturer means consistent supply chains and reduced delivery delays during critical shortages. Emergency preparedness improves substantially when institutions work with blood bag manufacturers offering rapid deployment capabilities. Additionally, comprehensive documentation and traceability features incorporated by professional manufacturers facilitate regulatory compliance and quality audits. Choosing an established blood bag manufacturer demonstrates institutional commitment to excellence in transfusion medicine and patient care standards.

Tips And Tricks

Second-gen antihistamine sourcing: how to distinguish EP/USP grades for cetirizine API?

08

Jun

Second-gen antihistamine sourcing: how to distinguish EP/USP grades for cetirizine API?

Sourcing high-quality cetirizine API requires pharmaceutical manufacturers to navigate complex regulatory distinctions between European Pharmacopoeia and United States Pharmacopeia standards. The choice between EP and USP grade cetirizine directly im...
View More
Rising pediatric anti-nausea market: collaboration opportunities for dimenhydrinate 25mg development.

01

Jul

Rising pediatric anti-nausea market: collaboration opportunities for dimenhydrinate 25mg development.

The pediatric anti-nausea pharmaceutical market is experiencing unprecedented growth as healthcare providers increasingly recognize the unique challenges of treating nausea and vomiting in children. While adult formulations like dimenhydrinate 50 mg ...
View More
FDA registration pathway and OTC monograph compliance for eye drop exports to the US.

17

Aug

FDA registration pathway and OTC monograph compliance for eye drop exports to the US.

Exporting lubricant eye drops to the United States requires a thorough understanding of FDA regulations, OTC monograph standards, and compliance pathways. Manufacturers seeking to market lubricant eye drops in the US must navigate a complex regulator...
View More
How to select slitting rewinder suppliers for paper, film, or nonwoven production lines?

08

Sep

How to select slitting rewinder suppliers for paper, film, or nonwoven production lines?

Choosing the right supplier for your rewinding or slitting machine is one of the most critical decisions you'll make for your production operation. Whether you run a paper mill, film conversion facility, or nonwoven manufacturing line, the quality an...
View More

Get a Free Quote

Our representative will contact you soon.
Name
Email
Tel
Company Name
Message
0/1000

blood bag manufacturer

Advanced Sterile Design and Collection Systems

Advanced Sterile Design and Collection Systems

Leading blood bag manufacturers incorporate sophisticated sterile needle and tube systems that facilitate efficient blood collection while maintaining absolute sterile integrity. The integrated collection apparatus eliminates multiple connection points that could introduce contamination, thereby significantly reducing bacterial transmission risks. A professional blood bag manufacturer designs these systems with ergonomic precision, enabling phlebotomists to complete collections safely and quickly. The double and triple bag configurations offered by quality manufacturers allow seamless component separation without breaking the sterile environment. Needle safety features prevent needlestick injuries while maintaining collection accuracy. The innovative design elements that distinguish top-tier blood bag manufacturers include smooth fluid flow, minimal air entrapment, and optimal anticoagulant distribution. These technical specifications directly impact blood quality, cellular preservation, and ultimate transfusion efficacy. Modern manufacturers continuously refine collection bag geometries to accommodate various blood volumes while maintaining standardized handling procedures across healthcare facilities worldwide.
Extended Shelf Life and Preservation Technology

Extended Shelf Life and Preservation Technology

A prominent blood bag manufacturer develops specialized preservation formulations and materials that extend viable storage periods significantly beyond traditional standards. Premium blood bags maintain cellular viability for forty-two days or longer, depending on specific anticoagulant and additive solutions selected by the manufacturer. The oxygen permeability of bag materials chosen by expert blood bag manufacturers ensures proper gas exchange, preventing metabolic complications during storage. Advanced plasticizers and PVC alternatives used in manufacturing prevent chemical leaching that could compromise blood components. Temperature monitoring strips integrated into quality bags help storage facility staff maintain optimal conditions consistently. The preservation technology perfected by established blood bag manufacturers reduces hemolysis rates substantially, ensuring patients receive maximum therapeutic benefit from transfusions. Rigorous testing protocols verify that each batch maintains preservation integrity throughout the designated shelf life. This commitment to extended preservation distinguishes reputable blood bag manufacturers, enabling healthcare facilities to manage inventory efficiently while reducing emergency procurement needs and associated costs.
Comprehensive Regulatory Compliance and Quality Assurance

Comprehensive Regulatory Compliance and Quality Assurance

Professional blood bag manufacturers maintain unwavering commitment to international regulatory standards, including FDA clearance, CE marking, and ISO certifications. Every production cycle includes rigorous quality control testing that verifies sterility, strength, and safety parameters established by regulatory agencies. A certified blood bag manufacturer implements comprehensive traceability systems enabling complete product documentation from manufacturing through patient administration. Advanced sterilization techniques, including gamma radiation and ethylene oxide treatment, ensure complete pathogen elimination without compromising product performance. Regular audits and documentation protocols maintained by responsible blood bag manufacturers demonstrate transparency and accountability. The manufacturer's quality assurance teams conduct accelerated aging studies and environmental stress testing to verify shelf-life claims accurately. Compliance certifications maintained by premium blood bag manufacturers provide healthcare institutions confidence in meeting transfusion medicine standards. Detailed batch records and certificate-of-analysis documentation from established manufacturers facilitate regulatory audits and institutional quality assessments seamlessly.

Get a Free Quote

Our representative will contact you soon.
Name
Email
Tel
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Name
Email
Tel
Company Name
Message
0/1000