paracetamol tablets factory
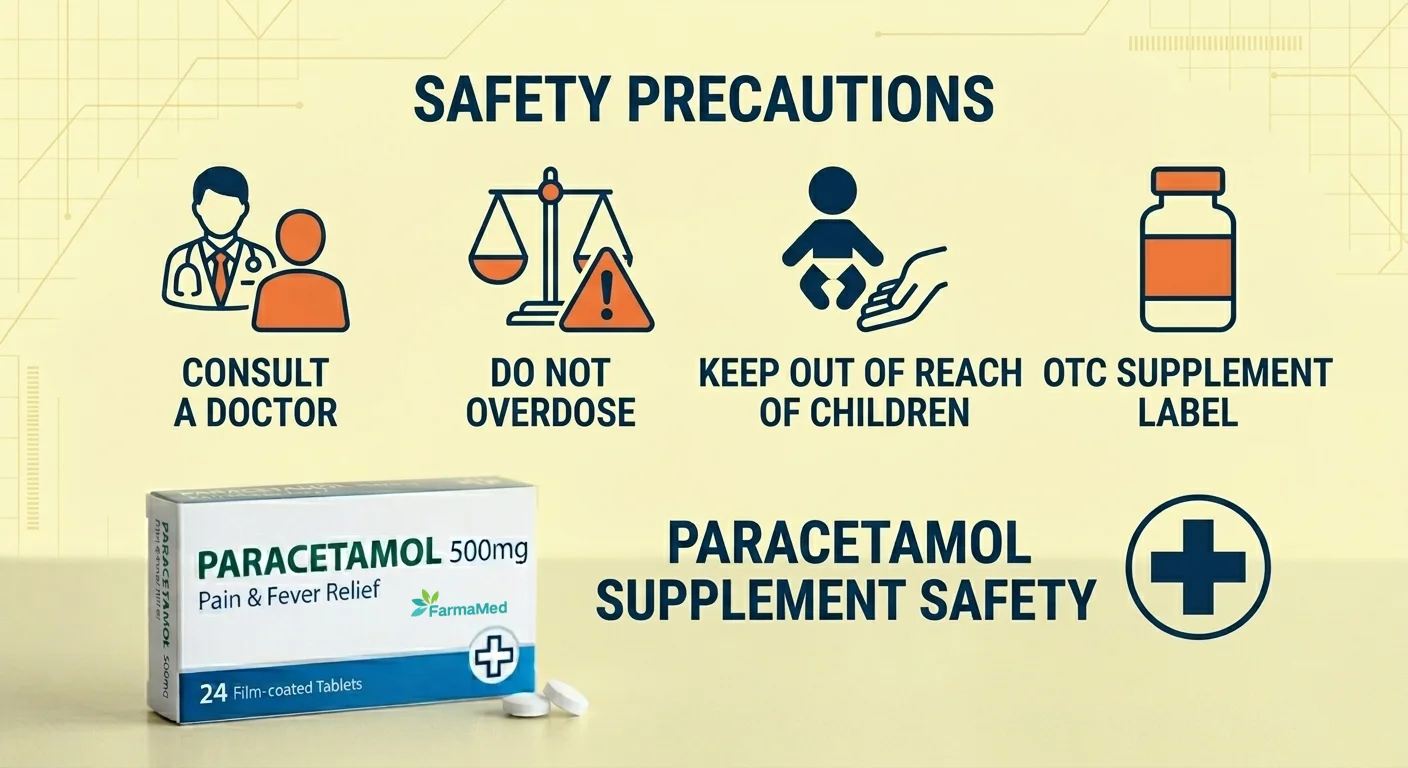
A paracetamol tablets factory represents a specialized pharmaceutical manufacturing facility dedicated to producing high-quality pain relief and fever-reduction medications. The paracetamol tablets factory operates as a comprehensive production center equipped with state-of-the-art machinery and quality control systems designed to meet international pharmaceutical standards. These facilities manufacture paracetamol tablets in various strengths, typically ranging from 325 mg to 650 mg, serving healthcare providers, distributors, and consumers worldwide. The paracetamol tablets factory utilizes advanced tablet compression technology, automated packaging systems, and rigorous quality assurance protocols throughout the production process. Main functions include raw material sourcing and verification, tablet formulation and compression, coating and polishing, packaging, labeling, and final quality testing. Technological features of a modern paracetamol tablets factory encompass precision machinery that ensures accurate dosage uniformity, moisture control systems that maintain optimal storage conditions, and computerized tracking systems for complete batch documentation. Applications for paracetamol tablets produced by the paracetamol tablets factory extend across hospitals, pharmacies, retail channels, and direct-to-consumer markets. These tablets effectively address common health concerns including headaches, muscle aches, minor arthritis pain, and fever management. The paracetamol tablets factory maintains strict compliance with Good Manufacturing Practices, ensuring every tablet meets stringent efficacy and safety standards. Production capacity varies significantly, with facilities ranging from small-scale operations producing millions of tablets annually to large industrial paracetamol tablets factory operations manufacturing billions of units. Modern facilities implement sustainable practices, efficient waste management, and eco-friendly processes. The paracetamol tablets factory sector continues evolving with innovations in formulation technology, faster dissolution rates, and improved bioavailability. These manufacturing centers support global healthcare demands while maintaining consistent quality, reliability, and cost-effectiveness that healthcare systems and consumers depend upon.
 EN