oral tablets manufacturer
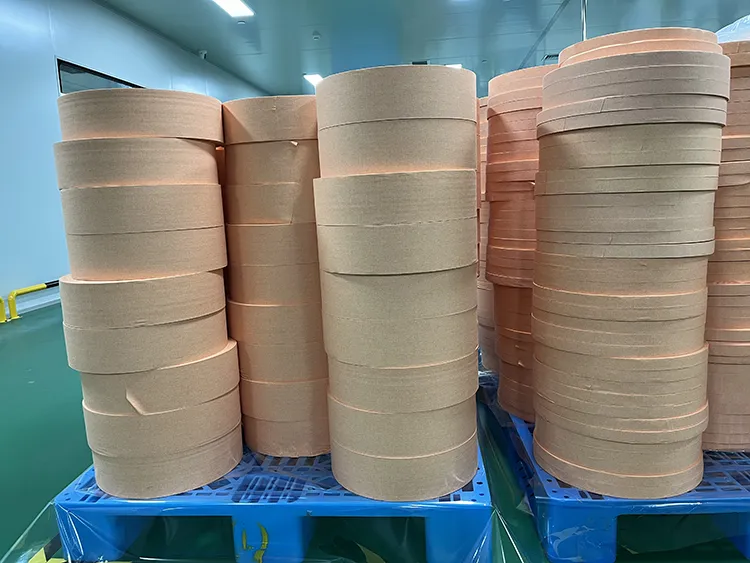
An oral tablets manufacturer specializes in producing pharmaceutical tablets designed for oral administration, serving as a critical player in the global healthcare supply chain. These facilities employ advanced pharmaceutical technology to create tablets that deliver active pharmaceutical ingredients directly through the digestive system. The oral tablets manufacturer utilizes precision equipment and quality control systems to ensure each tablet meets strict pharmaceutical standards and regulatory requirements.
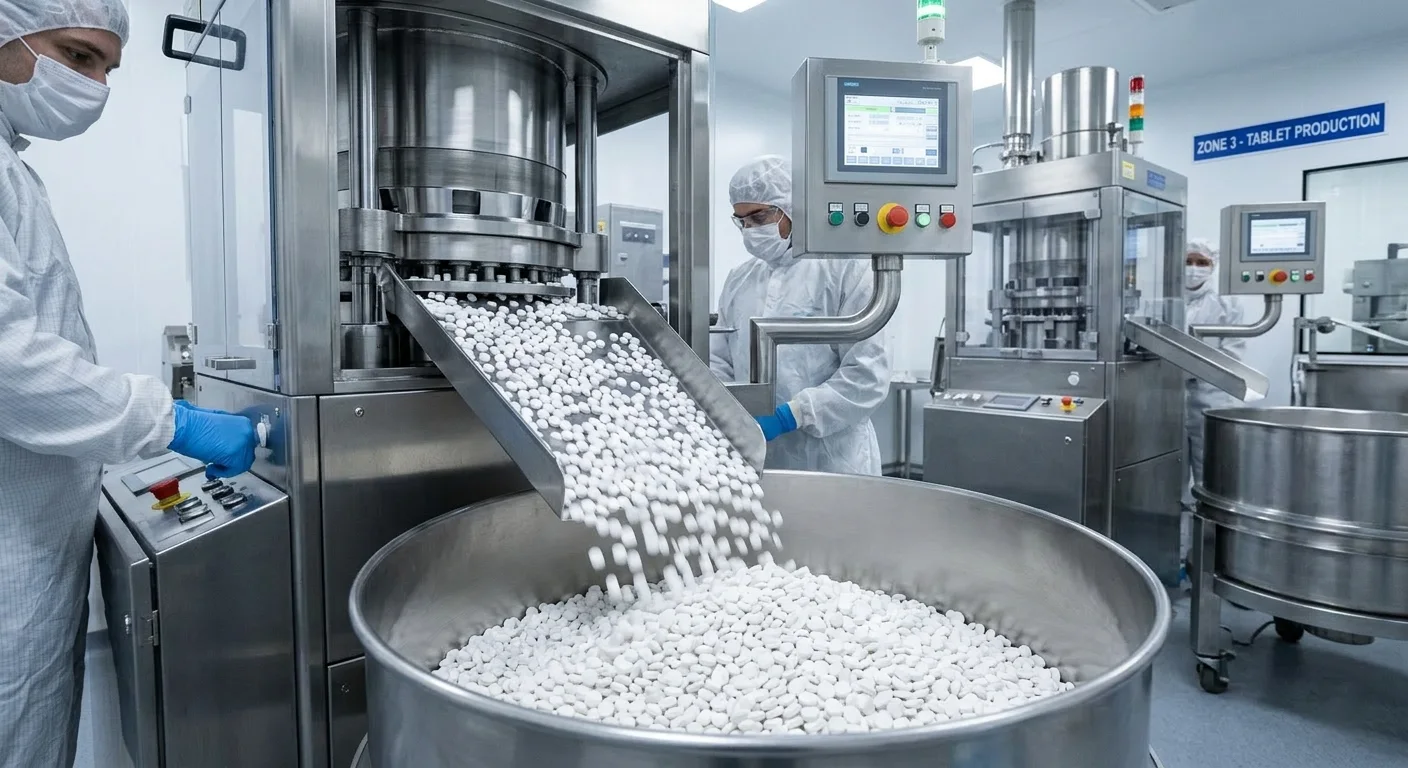
The primary functions of an oral tablets manufacturer encompass formulation development, tablet compression, coating, and packaging. These facilities transform raw pharmaceutical materials into finished dosage forms that patients can easily consume. Modern oral tablets manufacturer operations incorporate high-speed tablet presses, automated packaging systems, and comprehensive testing laboratories.
Technological features distinguish leading oral tablets manufacturer operations. These include continuous monitoring systems, moisture-controlled environments, and real-time quality assurance protocols. Advanced machinery enables consistent tablet weight, hardness, and dissolution rates, ensuring therapeutic efficacy.
Applications for products from an oral tablets manufacturer span multiple therapeutic areas including pain relief, antibiotics, vitamins, and chronic disease management. Healthcare providers, pharmaceutical companies, and retail pharmacies depend on reliable oral tablets manufacturer services to supply medications meeting patient demand.
The oral tablets manufacturer industry continues evolving with innovations in coating technologies, sustained-release formulations, and personalized medicine approaches. These advancements enable better patient outcomes and expanded treatment options across diverse medical conditions.
 EN