Get a Free Quote

Our representative will contact you soon.
Name
Email
Tel
Company Name
Message
0/1000
pharma tablets manufacturer-0

Home > 

pharma tablets manufacturer

A pharma tablets manufacturer specializes in producing high-quality pharmaceutical tablets through advanced manufacturing processes and rigorous quality control standards. These manufacturers serve as essential partners in the pharmaceutical industry, converting active pharmaceutical ingredients into finished dosage forms that patients rely on for their health and wellness needs. The primary function of a pharma tablets manufacturer involves formulating, compressing, and packaging tablets according to strict pharmaceutical regulations and customer specifications. This process requires precise equipment, expert knowledge, and adherence to Good Manufacturing Practice (GMP) guidelines. Modern pharma tablets manufacturers utilize state-of-the-art technology to ensure consistency, potency, and safety in every tablet produced. Technological features of contemporary pharma tablets manufacturers include automated compression machines, real-time monitoring systems, and advanced packaging equipment. These technologies enable manufacturers to maintain exact dosage uniformity, detect defects automatically, and scale production efficiently. Integration of data analytics and quality assurance software helps track every batch throughout the manufacturing cycle. Applications for tablets manufactured by a pharma tablets manufacturer span across diverse therapeutic areas including cardiovascular treatment, antibiotics, pain management, and chronic disease management. Tablets remain the most popular dosage form due to their convenience, stability, and ease of administration. A professional pharma tablets manufacturer can produce various tablet types, from simple single-ingredient formulations to complex multi-component compositions, meeting specific market demands and regulatory requirements globally.
New Product Recommendations

Choosing a reliable pharma tablets manufacturer offers numerous practical benefits that directly impact your pharmaceutical business success. Quality assurance stands as a fundamental advantage, as established manufacturers implement comprehensive testing protocols ensuring every tablet meets potency, purity, and safety standards before distribution. This commitment reduces risks and protects your brand reputation. Operational efficiency represents another significant benefit of partnering with an experienced pharma tablets manufacturer. These facilities streamline production processes through optimized workflows, reducing manufacturing timelines while maintaining exceptional quality. Faster turnaround times allow you to respond quickly to market demands and maintain competitive advantage in dynamic pharmaceutical sectors. Cost-effectiveness emerges as a compelling advantage when working with a professional pharma tablets manufacturer. Economies of scale, efficient resource management, and optimized production techniques translate directly into competitive pricing without compromising quality. This financial benefit improves your profit margins and market competitiveness. Flexibility and customization capabilities distinguish modern pharma tablets manufacturers from competitors. Whether you need small pilot batches or large-scale production runs, these manufacturers adapt to your specific requirements. They accommodate various tablet sizes, shapes, colors, and formulations, supporting your product differentiation strategy. Regulatory compliance expertise provides invaluable advantages when selecting a pharma tablets manufacturer. Established manufacturers maintain current knowledge of international standards, documentation requirements, and submission protocols. This expertise accelerates regulatory approvals and ensures your products meet all jurisdictional requirements. Long-term partnership benefits include consistent supply reliability and dedicated technical support. A committed pharma tablets manufacturer becomes an extension of your team, offering formulation advice, process optimization, and continuous improvement initiatives that enhance your overall pharmaceutical operations and market positioning.

Latest News

GMP certification landscape of global suppliers for cetirizine tablets 10mg.

15

Jun

GMP certification landscape of global suppliers for cetirizine tablets 10mg.

The GMP certification landscape for cetirizine tablets 10mg suppliers presents a complex regulatory environment where pharmaceutical manufacturers must navigate multiple international standards to ensure product quality and market access. Understandi...
View More
Winning hospital centralized procurement for folic acid 5mg: how to ensure 30M tablets annual supply?

26

Jun

Winning hospital centralized procurement for folic acid 5mg: how to ensure 30M tablets annual supply?

Securing a centralized procurement contract for folic acid tablets in hospital systems requires strategic planning, supply chain expertise, and deep understanding of healthcare procurement dynamics. When hospitals seek suppliers capable of delivering...
View More
How to verify eye drop sterility assurance through third-party test reports in B2B procurement?

10

Aug

How to verify eye drop sterility assurance through third-party test reports in B2B procurement?

Verifying the sterility and safety of lubricant eye drops is one of the most critical responsibilities in B2B procurement. When sourcing lubricant eye drops for clinical use, distribution, or institutional settings, relying solely on supplier claims ...
View More
How to select slitting rewinder suppliers for paper, film, or nonwoven production lines?

08

Sep

How to select slitting rewinder suppliers for paper, film, or nonwoven production lines?

Choosing the right supplier for your rewinding or slitting machine is one of the most critical decisions you'll make for your production operation. Whether you run a paper mill, film conversion facility, or nonwoven manufacturing line, the quality an...
View More

Get a Free Quote

Our representative will contact you soon.
Name
Email
Tel
Company Name
Message
0/1000

pharma tablets manufacturer

Advanced Manufacturing Technology and Precision Equipment

Advanced Manufacturing Technology and Precision Equipment

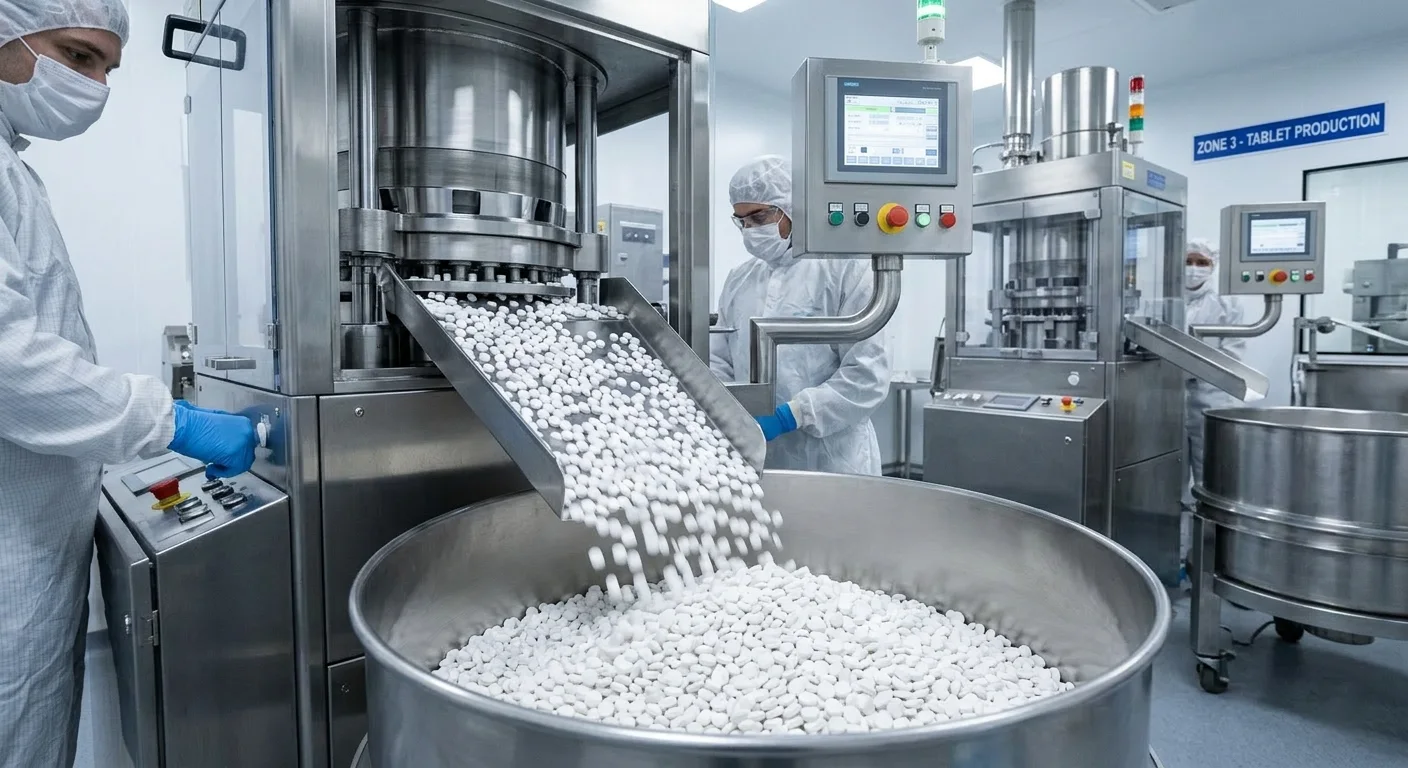
A leading pharma tablets manufacturer invests heavily in cutting-edge manufacturing technology that ensures exceptional precision and consistency in every production batch. Modern compression equipment delivers exact dosage uniformity, critical for maintaining therapeutic efficacy and patient safety. Advanced machinery monitors tablet weight, hardness, and thickness in real-time, automatically detecting and rejecting any tablets falling outside specification parameters. The technological infrastructure of a professional pharma tablets manufacturer includes automated production lines capable of producing millions of tablets daily while maintaining stringent quality standards. Integration of artificial intelligence and machine learning algorithms predicts potential equipment issues before failures occur, minimizing downtime and production interruptions. These innovations distinguish modern manufacturers in competitive pharmaceutical markets, enabling them to deliver superior products consistently. Automated packaging systems work seamlessly with production equipment, ensuring tablets are protected from contamination while meeting expiration dating requirements. This technological excellence directly translates into reliable supply chains and superior product quality that customers depend upon for pharmaceutical success.
Comprehensive Quality Assurance and Regulatory Compliance

Comprehensive Quality Assurance and Regulatory Compliance

A dedicated pharma tablets manufacturer maintains rigorous quality assurance protocols throughout every production stage, from raw material inspection through finished product release. Multiple testing layers ensure tablets meet all pharmaceutical standards including dissolution rates, stability profiles, and microbiological safety parameters. This comprehensive approach protects patient safety while building trust with healthcare professionals and regulatory agencies. Compliance with international standards represents a cornerstone advantage of working with an established pharma tablets manufacturer. These facilities maintain GMP certifications, ISO quality management systems, and regulatory approvals from major pharmaceutical bodies worldwide. Expert quality teams conduct stability testing, impurity analysis, and performance validation ensuring products meet or exceed all requirements. Documentation systems provide complete traceability for every batch, supporting regulatory audits and investigations. A professional pharma tablets manufacturer's commitment to compliance excellence eliminates uncertainties in pharmaceutical operations, allowing you to confidently market products knowing they meet all legal and safety requirements.
Customization Capability and Production Flexibility

Customization Capability and Production Flexibility

Modern pharma tablets manufacturers provide exceptional flexibility in accommodating diverse product requirements and market demands. Whether you need specialized tablet formulations, unique sizing, distinctive colors, or branding features, professional manufacturers possess capabilities to bring your vision to reality. This customization extends beyond physical characteristics to include complex formulation adjustments supporting your therapeutic objectives. Production flexibility represents another crucial advantage of partnering with an adaptable pharma tablets manufacturer. These facilities scale manufacturing volumes seamlessly, transitioning from clinical trial batches to commercial production runs without quality compromises. Short production lead times and responsive scheduling accommodate seasonal demand fluctuations and market opportunities. Technical teams collaborate closely with clients, offering formulation optimization suggestions and process improvements that enhance product performance. This collaborative approach ensures your tablets achieve optimal bioavailability, stability, and consumer acceptance while maintaining cost efficiency throughout product lifecycle.

Get a Free Quote

Our representative will contact you soon.
Name
Email
Tel
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Name
Email
Tel
Company Name
Message
0/1000